
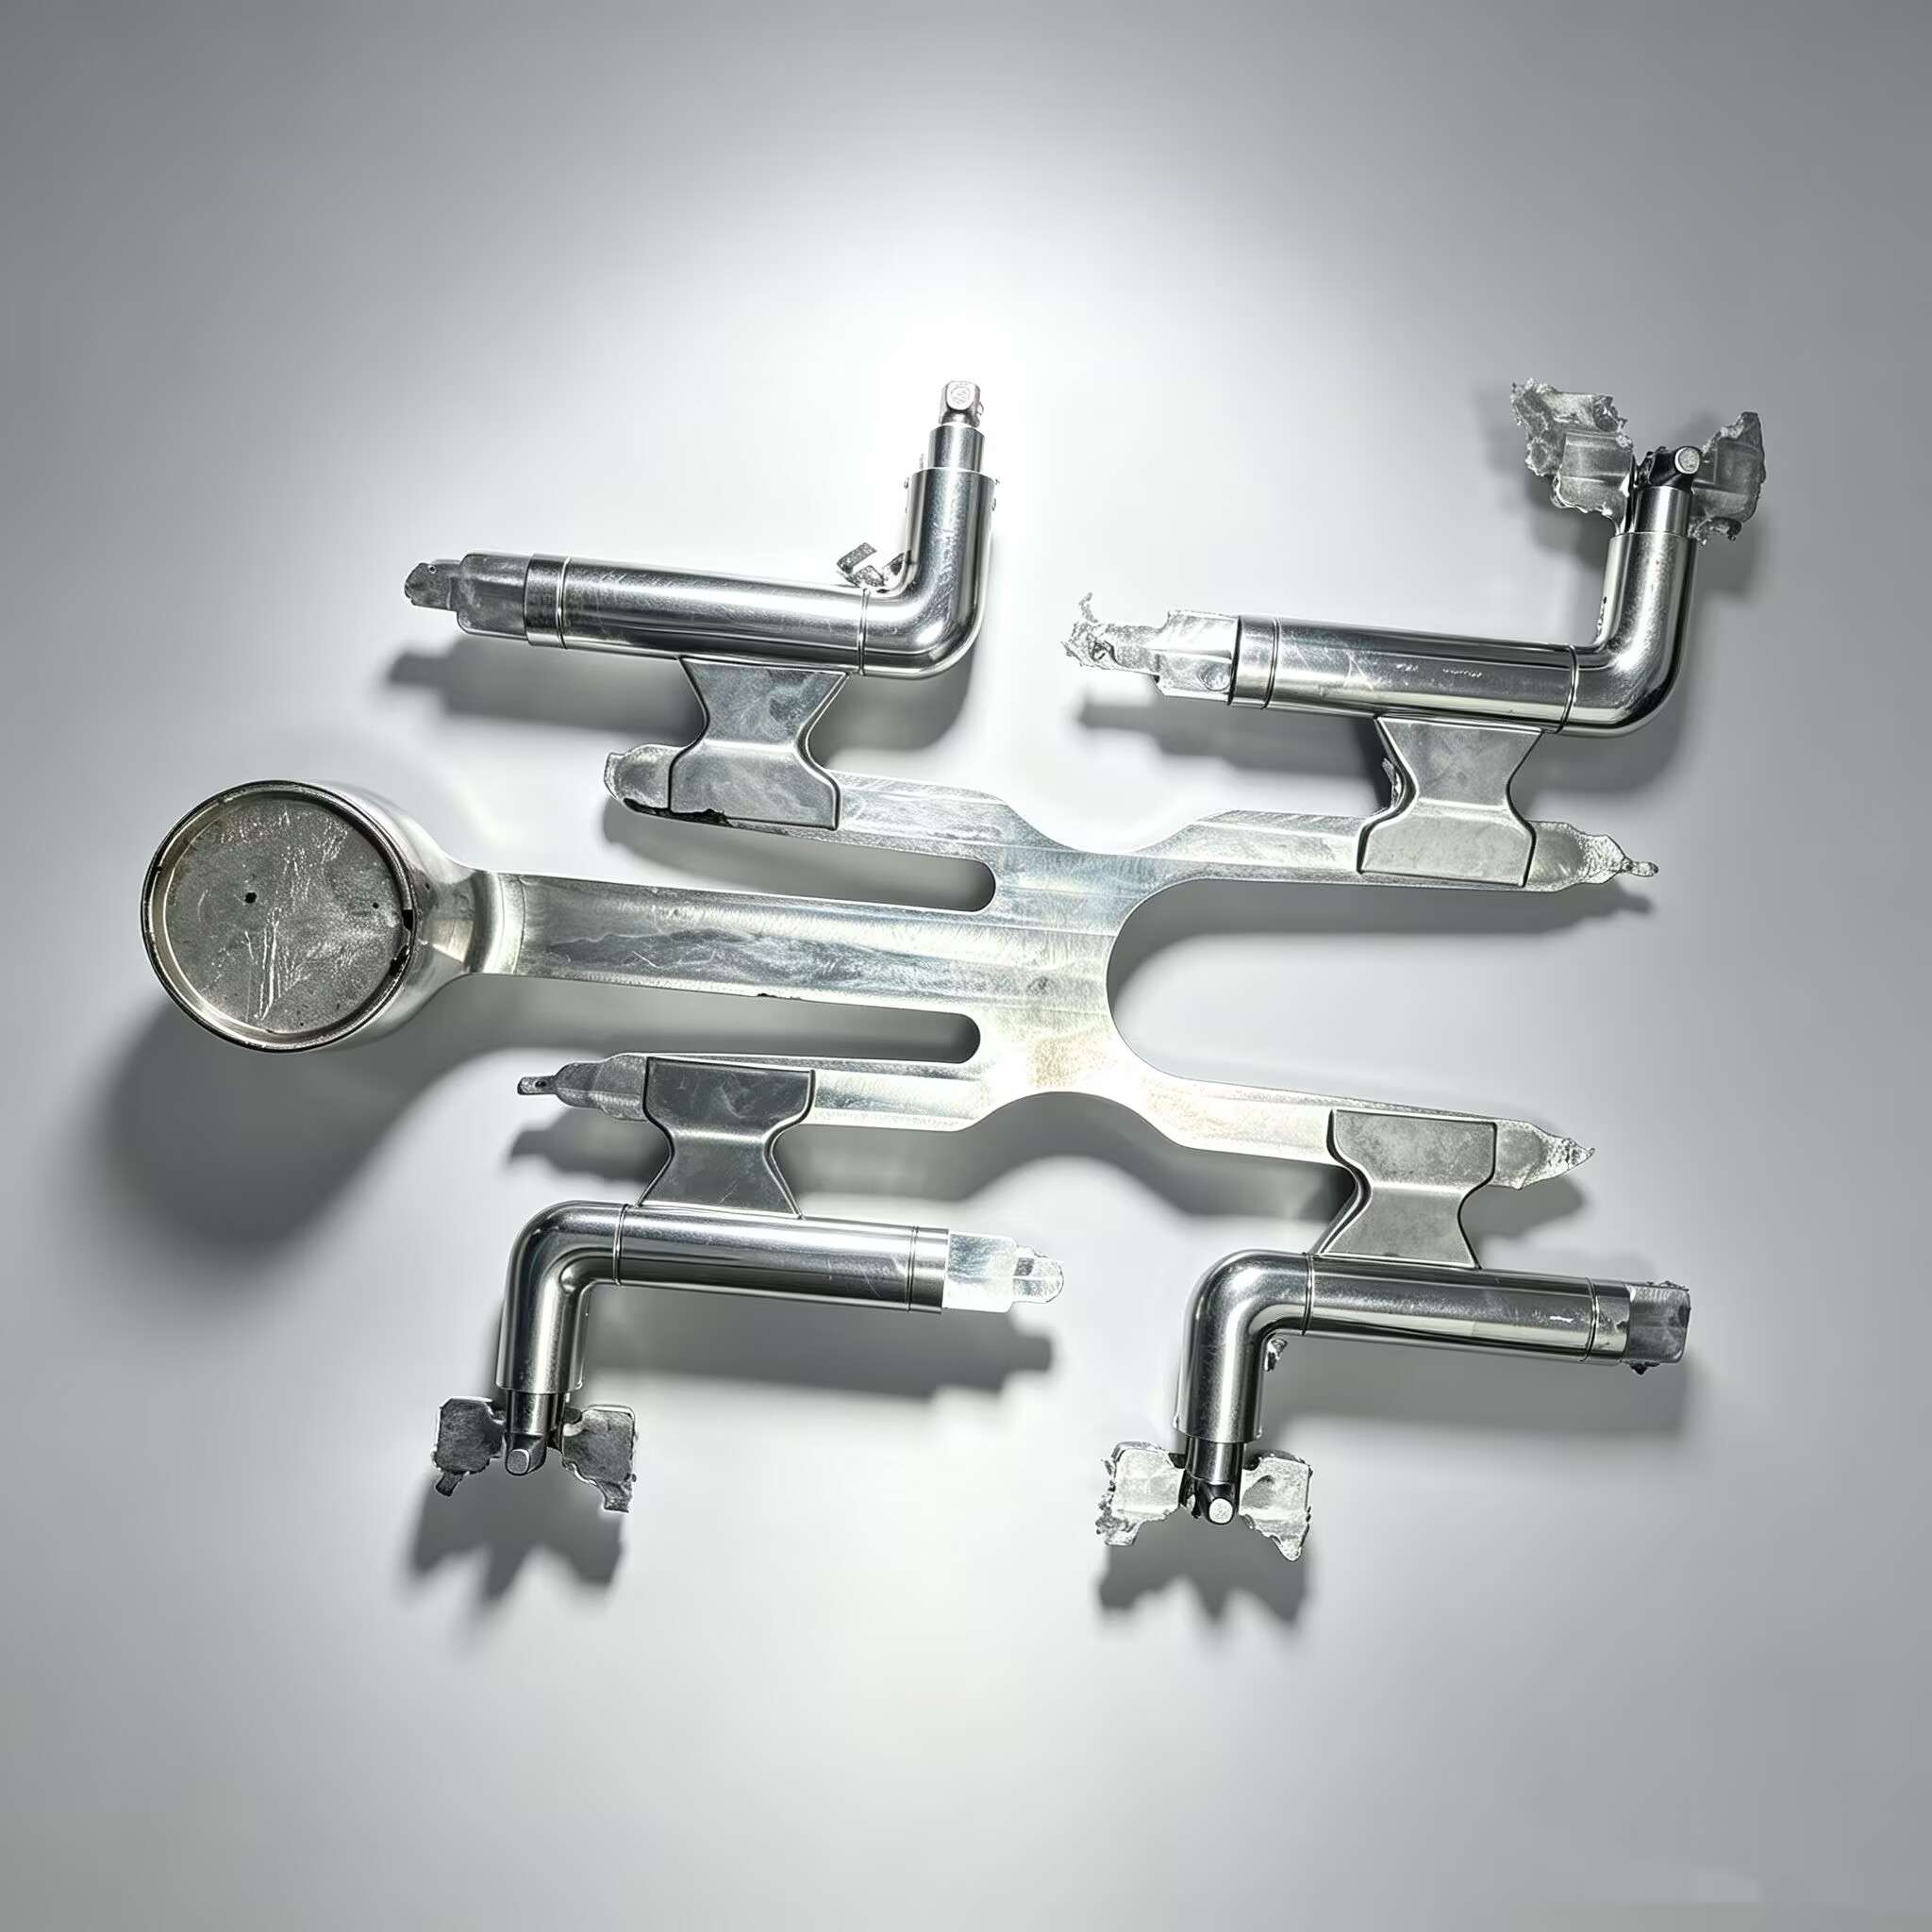

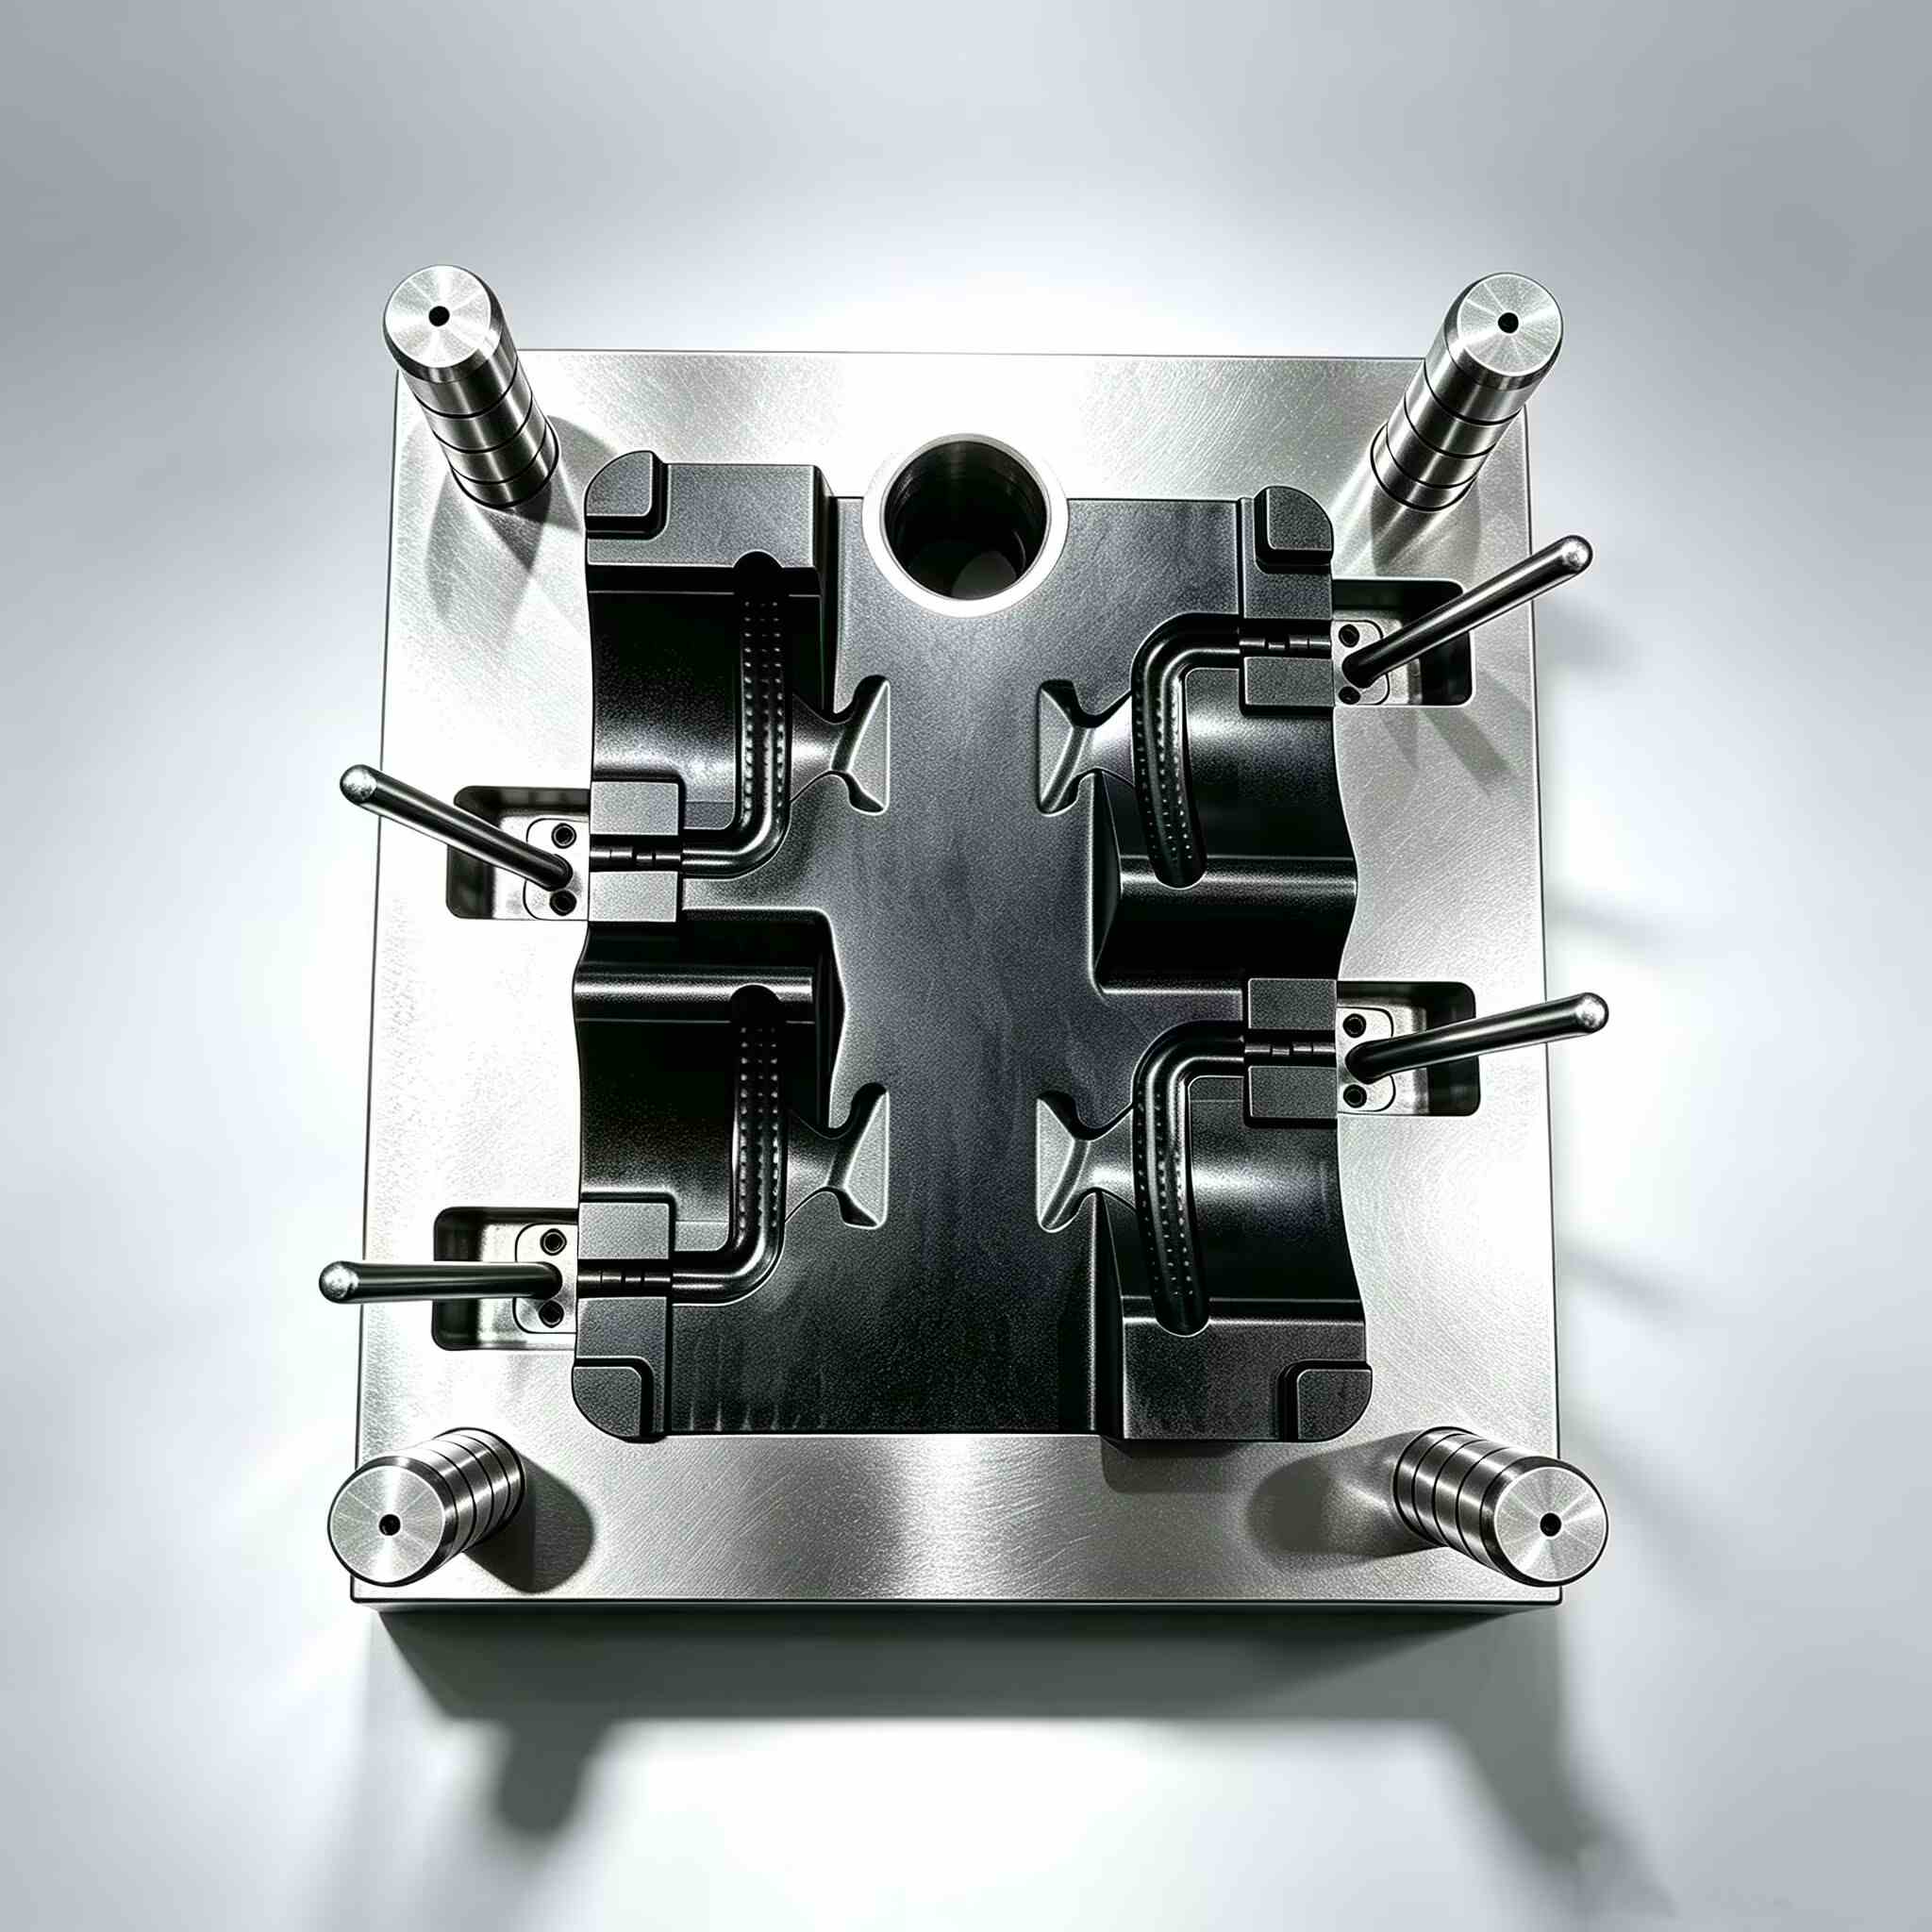
锌压铸模具零件
锌压铸是一种热室高压工艺,它将熔融的ZAMAK合金(通常为ZAMAK 3、5或8)以10-35 MPa的注射压力注入硬化钢模腔中。由于锌的熔点仅为380-420°C,远低于铝或镁,热室设计使注射系统始终浸没在熔融金属中,从而能够以每小时200-800次的频率对中小型零件进行注射。在XINKEY MOULD,我们采用与注塑模具相同的DFM(面向制造的设计)严谨性来设计锌压铸模具:在钢材切割之前,通过流动模拟规划浇口位置和流道平衡;根据零件几何形状优化冷却管路布局;并设计排气和溢流通道的尺寸,以便在注射行程的前15%内排出模腔气体。最终得到的模具能够生产出表面铸造一致、尺寸在不同生产批次间稳定的零件,标准项目的预计模具寿命为 30 万至 50 万次注塑,而采用优质 H13 和先进热处理工艺后,模具寿命可达 50 万次以上。
- 卓越的表面细节和尺寸精度
- 最薄壁设计——可薄至0.5毫米
- 适用于镀铬和装饰性表面处理
- 生产速度快——模具成本低
- 优异的耐腐蚀性和耐磨性
- 产品详情
1. 本产品可以解决哪些问题?
热室鹅颈管侵蚀和堵塞
在热室注塑机中,鹅颈管和喷嘴始终浸没在熔融锌合金中。在持续的工作温度下,锌铁金属间化合物会在鹅颈管表面积聚,导致注射重量漂移并最终堵塞。标准碳钢鹅颈管在大批量生产下会在 8-12 周内发生性能退化。XINKEY MOULD 指定使用氮化或陶瓷涂层鹅颈管表面,并设计冷却回路,将熔体温度维持在工艺设定点周围 ±5°C 的范围内,从源头上减少化合物的积聚。
电镀后的孔隙率和表面起泡问题
用于电镀或粉末涂装的锌铸件必须无气孔。铸件中残留的气体在高温固化或电镀过程中会膨胀,导致表面起泡,从而在精加工阶段造成零件报废。对于具有大面积平面的零件,标准的溢流和排气设计通常过于保守。XINKEY MOULD 利用流动模拟技术来确定最后填充区域,添加有针对性的溢流和真空辅助排气装置,并建议浇口速度在 30–50 m/s 之间——这是填充型腔而不产生湍流引起的气体滞留的最佳速度范围。
长薄壁零件弹出后的翘曲
ZAMAK合金在凝固过程中收缩率约为1.1%至1.3%。对于细长薄壁零件,型腔内冷却不均匀会产生残余热应力——零件在脱模后会发生弯曲或扭曲,无法满足平面度要求。XINKEY MOULD采用随形冷却管线来平衡厚薄截面的散热,在面向制造的设计(DFM)过程中模拟凝固和热应力分布,并在几何形状导致翘曲不可避免时建议使用铸后矫直夹具。
2. 典型应用
汽车内饰和外饰
门把手、后视镜外壳、车标底座、安全带组件和装饰边框。ZAMAK 3 和 5 可提供镀铬或 PVD 涂层所需的表面光滑度,符合汽车 A 级表面标准。
消费电子产品外壳和框架
智能手机中框、笔记本电脑铰链支架、耳机充电盒外壳和路由器底座。壁厚低至 0.5 毫米,并具有锌合金固有的电磁干扰屏蔽性能。典型零件重量:5–80 克。
锁具、五金件和卫浴配件
挂锁锁体、门锁芯、水龙头把手、淋浴喷头主体和家具铰链部件。锌优异的铸造性能使其能够制造出复杂的内部通道,用于容纳锁销和水道,并保持严格的铸造公差。
工业连接器外壳和紧固件
D-sub连接器外壳、气动接头本体、皮带扣框架和释放杆。具有良好的强度重量比和适用于承重部件的机械性能。ZAMAK 5的拉伸屈服强度为200–280 MPa。
玩具和收藏金属零件
压铸模型车车身、人偶底座、奖章和勋章。锌能够忠实地再现精细的表面细节——雕刻、纹理、小型标志——使其成为高精度装饰铸件的首选材料。
3. 规格表
| 物品 | 细节 |
| 流程类型 | 热室高压压铸 |
| 典型合金 | ZAMAK 3 (ZnAl4)、ZAMAK 5 (ZnAl4Cu1)、ZAMAK 8 (ZnAl8Cu1) |
| 零件重量范围 | 每枪1克 – 5公斤 |
| 壁厚 | 最小0.5毫米;典型值1.0-2.5毫米 |
| 铸造公差 | 标准精度为±0.05mm;关键特征精度可达±0.03mm |
| 腔体范围 | 1至8腔;提供单腔系列模具 |
| 模具钢 | H13(ESR 级)、8407、SKD61;优质:H13 ESR + 氮化 + PVD 涂层 |
| 冷却 | 保形挡板/鼓泡冷却 + 直通水管;薄壁工具采用油加热 |
| 表面光洁度(铸态) | 根据合金和腔体抛光情况,SPI等级为B-2至A-3。 |
| 霉菌寿命预期 | 30万-50万次射击(标准H13);50万次以上(优质钢材+PVD涂层) |
| 后期制作服务 | 振动去毛刺、振动精加工、喷丸处理、电镀(锌、镍、铬)、粉末涂装、电泳涂装 |
| 交钥匙方案 | 仅模具出口,或模具+系列零件供应 |
| 设计与验证 | DFM报告、流动+凝固模拟、T1样品及尺寸报告 |
4. 项目流程与质量控制
第一阶段:零件可铸造性审查和面向制造的设计
行动:分析三维CAD模型,确定拔模角度(内壁最小0.5°,外壁最小1°)、壁厚均匀性、肋壁比和倒扣几何形状。推荐浇口类型、浇口位置、溢流位置和分型线方向。
质量控制重点:DFM 报告:草稿分析热图、浇口位置及流动距离计算、估计注射重量和注射压力、循环时间预测。
第二阶段:流动模拟和热分析
行动:使用实际铸造工艺参数(熔体温度、注射速度、模具温度)运行 ZAMAK 合金流动模拟。识别最后填充区域和残余气穴。相应地设置溢流口和真空排气口。运行凝固模拟以预测缩孔率。
质量控制重点:模拟报告:薄壁零件的填充时间小于 40 毫秒,凝固梯度图显示向浇口/溢流方向的定向凝固,孔隙率概率图显示关键区域的孔隙率 <1.5%。
第三阶段:模具加工和热处理
行动:采用 H13 ESR 钢坯粗铣型腔和型芯。真空热处理至 HRC 46–48。消除应力。高速精铣,型腔表面步距为 0.01mm。电火花加工锐角和深肋。
质量控制重点:所有刀片均进行100%硬度测试:HRC 46–48。型腔尺寸检查:与三维模型相比误差为±0.01mm。型腔表面粗糙度Ra≤0.4μm。在10 bar水压下进行30分钟的水压测试。
第四阶段:模具组装及配合测试
行动:组装型芯、型腔、顶出系统和滑块。使用角度销或液压缸验证滑块的定时。检查顶针的长度和行程。安装热电偶以监测模具温度。
质量控制重点:装配检查清单:滑块运动顺畅,间隙为 0.02–0.04mm,顶出系统行程已验证,冷却回路流量测试,分型线匹配通过蓝勾(≥85% 接触)。
第五阶段:合作铸造厂的T1压铸试验
行动:将模具安装到热室压铸机上。设定工艺参数:熔体温度410–430°C(ZAMAK 3),注射速度,增压压力,冷却时间。运行50–100次以稳定工艺,然后连续抽取20次进行尺寸评估。
质量控制重点:尺寸报告:使用三坐标测量机 (CMM) 测量 5 个零件,所有关键尺寸均在公差范围内。对 2 个零件进行横截面切割:结构区域的孔隙率 < 1.5%。20 倍放大倍率下的表面检查:可见表面无冷隔,无流动痕迹。注射重量稳定性:20 次注射测量的变异系数 (CV) < 0.5%。
第六阶段:最终处理和交付
行动:对模具进行最终去毛刺、清洗和防锈处理。将模具装入熏蒸木箱。提供模具试模视频、工艺参数表、钢材证书和备件清单。
质量控制重点:客户所需文件:模具3D装配图、尺寸报告、工艺参数卡、钢材证书、终身备件包。零件采用PP袋+隔板包装发货。
5. 为什么选择新基模具
模具设计应以铸造实际情况为依据
大多数模具制造商在绘制压铸模具图时,从未真正接触过热室压铸机。而我们则直接与合作铸造厂对接。我们的工程师了解鹅颈喷嘴的对准公差、注射套筒的磨损模式,以及排气深度如何影响两万次注射过程中飞边的生长。这些实践经验贯穿于每一个浇口位置和溢流口尺寸的决策之中。
钢材接触轧机前的流动模拟
每个锌压铸模具项目都会进行 ZAMAK 专用流动和凝固模拟。我们不猜测气孔会出现在哪里——而是通过建模、设置溢流口来引导气流,并在 T1 阶段进行横截面取样来确认。这减少了传统模具制造流程中耗时数周的反复试错浇口位置调整。
H13 ESR钢材为标准配置——并非升级
许多供应商标称使用 AISI H13 钢材,但实际交付的却是等级较低的 H13 钢材,其内部含有碳化物带,导致在 5 万次注塑后出现热裂纹。XINKEY MOULD 的标准钢材为电渣重熔 (ESR) H13,并经过真空热处理和三次回火。对于使用玻璃纤维增强合金或磨损性环境的高磨损应用,我们提供型腔表面 PVD 涂层(CrN、AlCrN),以延长模具寿命。
交钥匙工程:一份合同,从模具到成品零件
您可以购买模具并在您自己的铸造厂进行生产。或者,您可以与我们签订模具及批量零件供应合同——我们负责模具制造、试模,并将成品零件交付到您的仓库。模具制造商和铸造厂之间无需交接,一位项目经理即可负责整个流程。
6. 常见问题解答
Q1:热室压铸和冷室压铸锌合金有什么区别?
热室压铸工艺将注射机构(鹅颈管和喷嘴)浸没在熔融锌液中,使其具有自吸功能,速度极快——典型循环时间为 3-8 秒。冷室压铸工艺则需要手动将熔融金属舀入或计量到注射套筒中,速度较慢,主要用于铝和镁的压铸。锌几乎总是采用热室压铸工艺,而这正是 XINKEY MOULD 所优化的工艺。
Q2:锌压铸件的壁厚可以做到多薄?
采用 ZAMAK 3 工艺和优化的浇口设计,我们能够使中小尺寸零件的壁厚低至 0.5 毫米。然而,实际最小壁厚取决于流动路径的长度——较长的流动路径需要更厚的壁厚才能在凝固前填充材料。我们在 DFM(面向制造的设计)过程中通过流动模拟进行评估,并针对您特定的零件几何形状推荐可实现的最小壁厚。
Q3:我可以直接从 XINKEY MOULD 获得镀铬锌零件吗?
是的。我们负责协调整个工艺流程:模具设计→铸造→去毛刺→抛光→电镀(锌、镍、铬)。模具设计充分考虑了电镀工艺——壁厚均匀以最大程度减少缩痕,接合处采用较大的圆角以避免镀层堆积,表面平整无流纹,避免镀铬层下显露出流纹。
Q4:锌压铸模具的典型使用寿命是多少?
标准H13模具在经过适当的热处理和定期维护(每3万至5万次注塑后进行一次氮化修补)后,可承受30万至50万次注塑。对于年注塑量超过50万次的连续大批量生产项目,我们推荐使用ESR级H13模具,并采用PVD涂层,这样可以延长模具寿命至50万次以上,并减少因翻新而造成的停机时间。
Q5:我想用锌压铸代替砂型铸造或重力铸造工艺——成本权衡是什么?
压铸模具的前期成本高于砂型模具,但单件成本大幅降低——年产量超过5000件时,通常比砂型铸造低60%至80%。锌压铸还具有更高的尺寸精度(±0.05毫米,而砂型铸造为±0.5毫米)和更快的生产周期,从而减少了在制品库存。我们可以在报价过程中针对您特定零件进行成本对比分析。
Q6:压铸模具报价需要发送什么文件格式?
3D CAD 文件(STEP 或 IGES 格式)以及包含公差、合金规格(通常为 ZAMAK 3、5 或 8)、年产量和任何铸后加工要求(电镀、粉末涂装、机械加工)的 2D 图纸。如果零件需要与其他组件组装,则需要提供装配图或配合零件数据,以便我们正确设计关键接口。
Q7:从模具订单到首批样品需要多长时间?
单腔锌压铸模具从设计定稿到T1样品制作通常需要5-7周。多腔模具或带有复杂滑块和型芯抽取装置的模具可能需要7-10周。我们会提供详细的项目时间表和报价,并在执行过程中每周分享进度照片。
产品





最新消息

- 23rd 10 月 2026
Low-Volume Injection Molding: On-Demand Production & Fast Tooling
Why does Low-Volume Injection Molding Fit Uncertain Demand?
Low-volume injection molding gives you a production path when demand moves. You can make saleable parts, validate a design, and learn from field use before committing to a large steel tool.
On-demand production lets you buy smaller releases, keeping cash and warehouse space tied to real orders. Aluminum tooling can bridge a prototype and stable production. The choice depends on geometry, resin, quantity, and change cost.
When does On-Demand Production Make Sense?
Use it for a new product with uncertain demand, irregular replacement orders, or planned design revisions. It suits medical, laboratory, smart hardware, and industrial products that need hundreds or a few thousand validated parts. The run can expose fit, assembly, and surface issues while tool changes remain manageable.
What does Fast Tooling Change?
Fast tooling compresses the time between a frozen CAD file and useful parts. A practical route combines a rapid tooling review, mold design, CNC machining, trial molding, and a T1 check. The goal is a controlled learning cycle. Aluminum tooling can suit early production and provide data for a later hardened mold.
How does the Process Control Tooling and Production Risk?
Low-volume injection molding production still needs production-grade thinking. A short run can hide a poor gate or unstable cooling layout, then repeat the problem as demand rises. Review the part, mold, and press together so each decision has a measurable reason.
What Happens in an Injection Molding DFM Review?
An injection molding DFM review checks wall thickness, draft, parting line, gate, venting, ejection, shrinkage, and press tonnage. Mold-flow simulation can show filling balance, air traps, weld lines, and cooling differences before steel is cut. This mold design for manufacturability step also flags undercuts that may need sliders, lifters, or inserts. Marked-up CAD views show the cost and schedule effect of each change.
How are Tooling and Samples Verified?
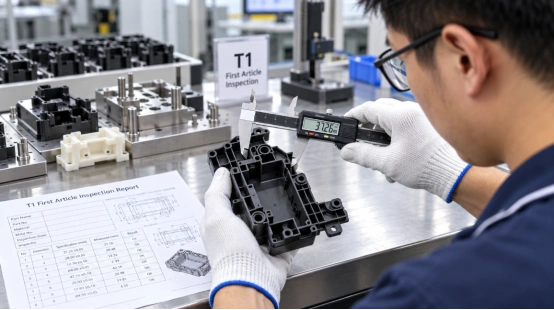
After machining, trial molding checks the cavity, runner, cooling, and ejection systems. Record T0 findings, correct root causes, and review T1 parts against the drawing. Ask for the inspection method, resin lot, and sample process conditions.
Which Quality Features Need a CTQ Plan?
Mark CTQ features where a dimensional shift affects sealing, fit, force, optics, or electrical safety. Link each CTQ to a gauge or CMM check, sampling frequency, and limit. This keeps a low-volume trial run useful for repeat orders and gives evidence beyond a visual sample.
Which Part Design Choices Affect Cost and Speed?
Part geometry sets much of your tooling cost before a purchase order. Design edits can shorten injection molding lead time, reduce secondary work, and simplify plastic injection mold maintenance.
How Much Draft Angle Do You Need?
Add a draft angle to faces that pull along the opening direction. Textured faces and deep ribs usually need more draft than smooth faces. Review the parting line with the ejection plan so the part stays on the moving side and leaves the cavity cleanly. This small check prevents drag marks, whitening, and stuck parts during sampling.
Why does Wall Thickness Matter?
Keep wall thickness as even as the function allows. A common starting range for many thermoplastics is about 1 to 3.5 mm, followed by a resin-specific review. Thick zones cool slowly and can create sink marks; thin zones can restrict filling. Use ribs, bosses, and gussets that support the part while keeping section mass compatible with the cooling cycle.
Where do Radii and Vents Help?
Use internal radii at corners to lower stress and match the cutting path of an end mill. Put vents near the end of melt flow so trapped air can leave. Good venting supports filling and reduces burn marks.
How should You Specify Surface Finish?
Choose the finish that matches function and viewing distance. A polished cavity adds hand work and schedule. A machined or light-texture finish may meet the requirement with a simpler tool. State the finish by area.
How should You Plan Quantity, Materials, and Tool Life?
Quantity planning connects your forecast to mold structure. Review the next 12 to 24 months, order pattern, and finished-goods cost before choosing cavity count or steel grade.
Is a Single-Cavity or Multi-Cavity Mold Better?
A single-cavity mold keeps early tooling and change work easier to control. A multi-cavity mold can lower the piece price when demand is steady, provided geometry and runner balance support even filling.
Family molds can combine related parts for a pilot production run, but each cavity needs its own inspection limits. Ask for a cycle-time and capacity comparison, then select cavities with demand in view.
Which Material Fits a Bridge Production Run?
Select resin by strength, heat, chemicals, color, and regulatory need. PP, ABS, PC, PA, POM, and filled grades differ in shrinkage and cooling. Share the final material early so gate, vent, cooling, and steel decisions match it.
When should You Move to a Hardened Tool?
Move when demand, wear, or dimensional stability justifies the capital. Aluminum tooling can carry early on-demand production and design learning. A hardened steel mold fits a repeat program with higher shot counts, tighter process windows, or long service expectations. Keep the CAD, inspection data, and approved process settings from the first tool so the next tool starts with evidence.
What should You Ask a Supplier Before Ordering?
Your supplier conversation should end with numbers, documents, and named owners. The checklist below helps you compare a quote by total project risk and tooling cost.
Which Questions Clarify the Real Schedule?
Ask for DFM timing, tool build days, first trial date, correction allowance, sample quantity, and the expected injection molding lead time. Confirm who approves material substitutions and how an engineering change affects the quote. A supplier that supports low-volume trial production should also explain how it will scale to small-batch production or bridge production after approval.
Which Records Support a Purchase Decision?
Request the DFM report, mold-flow findings when used, steel and heat-treatment records, CTQ dimensional reports, and the T1/T2 issue list. Ask how cooling, venting, ejection, and wear parts will be checked. These records support tool release.
Where Can Engineering Support Shorten the Route to Production?
For projects that need both rapid tooling and a low-volume injection molding production plan, XINKEY MOULD works from the product-design stage through DFM, mold design, machining, trial molding, and small-batch production. Its engineering workflow covers wall thickness, draft angle, gate and runner balance, flow analysis, cooling, venting, and ejection before tooling starts.
The team also handles sliders, lifters, inserts, threaded cores, and two-shot structures when the part needs them. Multi-stage machining checks and trial-molding verification create a traceable handoff into pilot production. If you need to compare a rapid prototype mold with a production-ready plastic injection mold, share the CAD file, resin, CTQ features, expected quantity, and target date so the quote reflects the actual decision.
FAQ
Q1: What is low-volume injection molding used for?
A: It produces saleable parts for design validation, market testing, replacement demand, and early production before a larger tooling investment.
Q2: How does aluminum tooling affect fast tooling?
A: Aluminum tooling supports quick machining and practical revisions for early runs. Tool life and resin choice still need a project-specific review.
Q3: What information should you send for an injection molding DFM review?
A: Send the 3D CAD file, 2D drawing, resin and color, annual and first-run quantity, CTQ dimensions, finish callouts, and target date.
Q4: How long is the injection molding lead time?
A: It depends on geometry, mold structure, material, inspection needs, and revision rounds. Ask for separate dates for DFM, tool completion, T1 samples, corrections, and shipment.
Q5: When does a multi-cavity mold make sense?
A: It fits steady demand where balanced filling and shared inspection controls can lower the part cost. A single-cavity tool often suits early learning and changing designs.

- 22nd 10 月 2026
5 Benefits Of Rapid Tooling For Automotive Injection Molding
Car projects frequently shift. This usually happens once an initial physical part goes into a dashboard, console, lamp housing, or battery assembly. Rapid tooling for automotive injection molding offers a quick, manageable route. It takes you directly from CAD data to working parts.
These tools might rely on aluminum or soft steel. The exact metal depends on your target volume and chosen resin. The goal remains highly practical. You get to evaluate the piece and process. Plus, you can verify purchasing choices before paying for an expensive, long-lasting production tool.
What Is Rapid Tooling for Automotive Injection Molding?
It acts as a distinct mold-creation method. It fits automotive prototype production and medium-batch runs perfectly. A basic mold utilizes fewer cavities. It also features a very standard ejection setup.
Conversely, standard production molds require tough hardened steel. They need intricate slides, lifters, and balanced runners. Your final choice relies heavily on volume, geometry, resin, visual requirements, and strict delivery deadlines.
1. Faster Structural Changes Before Steel Commitment
The first physical sample exposes decisions that a screen can hide: a rib may interfere with a connector, a draft angle may hold the part on the wrong side, or a gate mark may land on a visible surface. A rapid prototype mold gives your design team a short feedback loop. You can review T1 samples, record the change, and update the part or mold while the project is still flexible.
How Does the Review Work?
Ask for DFM analysis before machining begins. The review should cover wall thickness, draft, parting line, undercuts, ejection, shrinkage, and the intended press.
The engineering record should also show which change affects tool cost, cycle time, or assembly fit. This makes a quote useful for purchasing because you can compare the cost of a revision with the cost of carrying a risky feature into production.
2. Earlier Validation of Automotive Plastic Parts
Automotive rapid injection molding lets you test structural features with a real molded part. Deep cavities, thin walls, ribs, bosses, and snap fits behave differently under filling, packing, cooling, and ejection. A digital model can guide the review, yet a physical sample still needs fit checks, load checks, surface review, and dimensional measurement.
Where Does Mold Flow Analysis Help?
Mold flow analysis maps gate position, runner balance, filling pattern, weld lines, air traps, shrinkage, and warpage and sink marks before steel is cut. The result is a mold design validation record that points to a specific action, such as moving a gate, changing a rib, adding a vent, or adjusting a cooling circuit.
For complex mold structures, this early work reduces the chance of discovering a slider, lifter, or insert problem during a late trial.
3. Better Control of Prototype Spending
Prototype tooling turns a large tooling decision into staged purchasing. You can order a defined quantity for fit, durability, and user testing, then decide whether the geometry merits a production tool. This fits projects that need low-volume injection molding for a pilot build, a customer trial, or a limited vehicle release.
What Should Purchasing Compare?
Compare the tool price with revision cost, resin usage, inspection time, machine size, and the value of the parts being tested. Ask whether the tool can be modified, whether wear parts are replaceable, and which dimensions will be measured on each sample.
A low entry price loses its value when the tool cannot support the next test or when every change requires a new build. A clear inspection plan also helps engineering, quality, and purchasing agree on the release decision.
4. Shorter Lead Times for Testing and Launch Decisions
Rapid tooling for automotive parts can move first shots into a working press in days or a few weeks, depending on geometry, material, and tool construction. CNC-machined aluminum or soft tooling often suits an early run. The supplier still needs time for design review, machining, assembly, trial molding, and corrections, so a realistic schedule matters more than a headline number.
Which Process Details Affect the Schedule?
Injection molding cycle time depends heavily on wall thickness, resin, mold temperature, and cooling layout. Well-planned mold cooling channels remove heat from thick areas and reduce the wait before ejection. Venting, runner balance, and a stable ejection system also affect the number of trial loops. When you request a quote, ask for milestones for DFM approval, steel release, first trial, dimensional report, and sample shipment.
5. A More Practical Mass Production Transition
Rapid tooling can use production-grade plastics, so the samples can represent the mechanical behavior, appearance, and assembly feel expected from the final part. The tool itself may have a shorter service life than a hardened production mold. That distinction should be written into the sourcing plan.
How Do You Plan the Handover?
Carry the approved CAD revision, resin grade, shrinkage data, gate location, cooling notes, and inspection results into the automotive injection molding tooling package.
A multi-cavity mold may need a new runner balance study and a different press condition. Treat the prototype run as process learning: record fill time, packing, cooling, ejection, and key dimensions. Those records shorten the mass production transition and give the production team a starting process window.
What Should You Look for in a Rapid Tooling Partner?
The practical value of a rapid tool comes from decisions made before cutting steel. XINKEY MOULD uses an engineering-first workflow that starts with DFM analysis and mold flow analysis, then moves through mold design, precision machining, trial molding, and verification.
Its team includes 22 in-house designers, with support for rapid T1 samples, low-volume injection molding, sliders, lifters, inserts, hot or cold runners, and cooling-system design. The automotive workflow includes an IATF-aligned process and PPAP documentation available on request.
For buyers comparing suppliers, the useful question is whether the same team can carry approved changes into production tooling. Its injection mold engineering solutions cover that design-to-sampling handoff and keep the release record tied to the mold revision.
FAQ
Q1: What is rapid tooling for automotive injection molding used for?
A: It produces early automotive plastic parts for fit checks, functional tests, pilot builds, and market or customer review before a long-life production mold is released.
Q2: When should you request DFM analysis?
A: Request DFM analysis before steel machining. Review wall thickness, draft, parting line, gates, ejection, cooling, shrinkage, and press requirements while design changes remain manageable.
Q3: Can rapid tooling support PPAP documentation?
A: The supplier can prepare PPAP documentation when the project quality plan calls for it. Confirm the required records, dimensional reports, material certificates, and process data before the first trial.
Q4: How fast can a rapid prototype mold deliver T1 samples?
A: A simple tool may reach T1 samples in days or a few weeks. Geometry, resin, tool material, cavity count, and the number of trial corrections set the actual schedule.
Q5: Does rapid tooling replace a production mold?
A: It supports prototype and bridge quantities. A hardened production mold is usually required for high shot counts, multi-cavity output, tight process control, and long service life.

- 15th 10 月 2026
5 Strategic Benefits of Outsourcing Rapid Tooling
A launch date can slip long before the first molded part. The delay often starts with a wall thickness that traps heat, a weak draft angle, or a late gate decision. Outsourcing rapid tooling puts engineering, machining, trial molding, and measured samples on one project path.
A capable tooling supplier connects speed with part quality and a credible route to production through rapid tooling services.
Benefit 1, Shorten Your Time to Market
Rapid tooling compresses the work between a released CAD file and a tested molded part. Engineering review, material planning, mold design, and machine scheduling can start from the same controlled data set.
Run Design and Manufacturing Work in Parallel
An outside team can review draft, wall thickness, undercuts, parting lines, gate position, ejection, and cooling while your product team closes cosmetic details. That overlap may remove several handoffs. It also gives procurement one schedule covering tool design, machining, assembly, trial, inspection, and sample shipment.
Set a Clear Sample Milestone
Ask the supplier to quote a date for T1 samples and list the inputs that control it. Standard tools may reach T1 in two to four weeks. Unscrewing or two-material tools can take four to eight weeks. Complexity, steel choice, bought-in components, and CAD changes still affect time to market.
Benefit 2, Turn Tooling Cost into a Controlled Project Budget
Internal tooling requires design hours, CNC and EDM capacity, assembly skill, press time, metrology, and corrections. Outsourcing places those items inside a defined project scope for comparison against launch volume.
Compare the Full Cost of Ownership
Compare quotations by total project cost. Repeated sampling, steel welding, long cycles, and early wear all add expense. Ask each tooling supplier to state the mold steel, expected life, cavity count, runner type, replaceable wear parts, inspection scope, trial rounds, and change policy.
Match the Tool to Expected Volume
A rapid prototype mold can use a simpler layout and steel suited to design validation or an early market run. A production tool needs balanced cooling, durable sliding parts, controlled hardness, and maintenance access. Share annual volume and likely product revisions before the quote.
Benefit 3, Find Design Risks Before Steel Is Cut
Small CAD choices can create large tool changes. Thin ribs may fill poorly, thick bosses can sink, limited draft can mark the surface, and an undercut may require a slider or lifter. Early engineering review gives you time to change the part file while the change is still simple.
Review the Part through DFM
A useful DFM analysis marks wall thickness, draft, shutoffs, parting lines, ejection points, tolerances, surface requirements, and assembly interfaces. It should also explain why each item matters.
For example, keeping a concentric bore on one mold half reduces mold-shift and tolerance-stack risk. A purchasing team can then approve the tool scope with visible technical reasons.
Test Flow, Cooling, and Warpage Digitally
Mold flow analysis can compare gate positions, pressure, weld lines, air traps, shrinkage, cooling, and warpage before machining. Moving a gate 5 mm in a simulation is a short task. A change after steel cutting can require welding, machining, polishing, and another trial.
Benefit 4, Validate Materials with Production-Like Parts
A printed prototype answers fit and appearance questions. It rarely reproduces resin flow, fiber orientation, shrinkage, weld lines, sink, or ejection behavior from molding. Rapid injection molding gives you parts made with the intended resin and a process close to the planned production method.
Test the Resin in the Intended Process
Use molded samples to compare candidate resins for stiffness, impact, heat, chemical exposure, sealing, color, and surface finish. Process details matter. Phenolic materials, for example, require controlled mold heat and effective venting. Insert-molded parts need secure insert location under injection pressure. Two-material parts need a sound bonding interface and accurate tool alignment.
Use Measured Samples for Decisions
Define the sample plan before the tool trial. Record resin grade, drying condition, melt and mold temperatures, pressure, cycle time, and cavity number. Then inspect critical dimensions and run the product tests that decide release.
A nice-looking sample can still hide a weak process window. Measured evidence gives engineering and purchasing the same basis for approval.
Benefit 5, Create a Practical Bridge to Mass Production
The first acceptable shot proves that the tool can make a part. Pilot runs test repeatability across cavities, shifts, and material lots. Outsourcing rapid tooling delivers the planned value when one team carries the project through sampling and early production.
Stabilize the Process during Pilot Runs
Low-volume production and bridge production let you supply launch units while the team checks cycle time, scrap, dimensional drift, assembly fit, packaging, and maintenance needs. Engineers can tune cooling, venting, packing, and ejection with direct access to the tool. That continuity matters when a defect appears only after a longer run.
Protect Return on Tooling Investment
Earlier sales help recover the tool investment, though repeatable output drives the larger return. Review yield, labor content, resin use, cycle time, press tonnage, and wear-part access. A parting-line choice that lowers projected area may allow a smaller press. A hot runner may cut runner waste at high volume. Each decision should connect to your forecast and unit-cost target.
What Should You Expect from an Engineering-Led Tooling Partner?
The five benefits depend on one connected engineering record from DFM through trial molding. XINKEY MOULD assigns 22 in-house designers to product review, mold design, and mold flow analysis. Its documented process covers wall thickness, draft, parting lines, sliders, lifters, cooling, venting, ejection, and material selection before machining. High-precision CNC work reaches ±0.01 mm-level control, and molding equipment spans 90T to 750T for sampling and production handoff.
For a buyer, the useful point is continuity. The same project can move from a 24-hour DFM report to tooling, T1 inspection, pilot quantities, and injection mold manufacturing. That structure makes design changes, sample findings, and production settings easier to trace. You can request a project review with the CAD file, resin, annual volume, finish, tolerance, and target sample date.
FAQ
Q1: When Should You Outsource Rapid Tooling?
A: Outsource when your launch plan needs molded parts sooner than your internal engineering, machining, or press capacity allows. It also suits projects that need DFM, material trials, or a direct path into pilot production.
Q2: What Files Should You Send for a Rapid Tooling Quote?
A: Send a 3D CAD file, a dimensioned drawing, resin grade, surface requirements, critical tolerances, annual volume, target tool life, and the required T1 date. Add assembly data when mating parts control fit.
Q3: How Can You Compare Tooling Quotes Fairly?
A: Compare steel, cavities, runner system, mold standard, expected life, inspection scope, trial rounds, sample quantity, change terms, lead time, and shipping. A line-by-line comparison reveals what each price includes.
Q4: Can Rapid Tooling Use Production Resin?
A: Yes. A suitable mold can run production resin for functional, dimensional, and assembly tests. Confirm drying, processing temperature, shrinkage allowance, and any fiber or flame-retardant content before tool design.
Q5: Can a Rapid Tool Move into Mass Production?
A: Some tools can support continued production when their steel, cooling, cavity layout, wear parts, and press interface match the volume target. Ask the supplier to state the expected shot life and maintenance plan in the quote.
- 16th 10 月 2026
The Strategic Advantages of Short-Run Injection Molding for Complex NPI
Complex new product introduction (NPI) projects rarely fail because the CAD model looks wrong. They fail when a part reaches steel, trial molding exposes a gate or cooling issue, and the schedule has no room for another tooling loop.
Short-run injection molding gives you production-like parts early. You can check fit, function, finish, assembly, and customer response before a full-volume tool absorbs the budget.
What Does Short-Run Injection Molding Add to NPI?
Short-run injection molding uses a production-intent mold and a controlled quantity of parts for design validation, pilot production, or bridge production. The run can be sized around a test plan, such as 100 parts for assembly checks or several thousand parts for a market release. Molded parts and process data provide the evidence for the next tooling decision.
A Physical Test of the Product
Resin shrinkage, weld lines, ejection marks, and actual assembly loads appear in molded parts. A printed model cannot show how a thin wall fills or how a snap fit behaves after cooling. Early molded samples let your team record dimensional data and make a change while the tool remains practical to modify.
A Bridge Between Design and Volume
Bridge production gives you sellable or field-test units while the final multi-cavity tool is being completed. This matters for a new medical accessory, smart device housing, or industrial enclosure with a fixed launch date. The same material family, gate concept, and process window can carry the project into the next tool stage.
Which NPI Risks Can You Control before Full-Volume Tooling?
The largest NPI costs often come from late engineering decisions. A short run creates a checkpoint for the decisions that affect tooling cost, yield, and delivery.
Part Design and DFM Analysis
Start with DFM analysis before cutting steel. Review wall thickness, draft angles, ribs, bosses, undercuts, parting lines, and the projected area that drives press tonnage. A small change to a rib or draft can remove a difficult slide, simplify machining, and reduce a later mold revision.
Flow, Cooling, and Ejection
Moldflow analysis can compare gate positions, runner balance, filling patterns, air traps, and weld lines. Cooling channel layout matters because cooling often occupies about 70% of an injection cycle.
Uneven thermal balance creates sink marks and warpage. Venting gives trapped gas a path out, while a balanced ejector pin, sleeve, lifter, or air-ejection system protects cosmetic surfaces during release.
Complex Geometry and Tolerance
Sliders, lifters, inserts, threaded cores, and two-shot features add movement and tolerance stack-up. A short-run tool lets you inspect those interfaces under real pressure. Check core and cavity alignment, guide pins, runner balance, and the fit of mating features before you commit to a larger cavity count.
How Should You Compare Short-Run Tooling Cost with Production Tooling?
Price the decision across the whole NPI path. A low quote becomes expensive when it creates extra sampling, hand rework, scrap, or a rebuild. A practical sourcing review should include tool steel, machining, trial molding, material waste, engineering time, freight, and the cost of a delayed launch.
Use Volume and Risk Together
Choose a cavity count that matches the validation need. A single-cavity or low-cavity mold can provide fast feedback for a complex enclosure. A multi-cavity tool makes sense after dimensions, resin, and assembly have settled. For high-cycle projects, steel selection and heat treatment affect wear parts, maintenance, and stable output.
Set Acceptance Data Before the Run
Define critical dimensions, cosmetic zones, cycle time, part weight, flash limits, and assembly tests before ordering. Ask for T1 samples, a measurement report, and a short list of open issues. This gives procurement a clear release gate and gives engineering facts for the next tool decision.
What Does a Reliable Short-Run Process Look Like?
The process should connect design review, mold design, machining, trial molding, pilot production, and mass production. Each handoff needs an owner and a measurable output.
A Practical Sequence
Share the 3D data, resin, annual volume, key dimensions, and launch date.
Complete DFM analysis and review Moldflow findings with the design team.
Select the parting line, runner, cooling, venting, ejection, and mold steel.
Machine and assemble the tool, then run T0 or T1 samples.
Measure parts, test assemblies, and record process settings.
Correct the tool or part design, then release a controlled pilot production run.
This sequence keeps the evidence close to the decision. It also makes a handoff to a higher-cavity tool easier because the team has a record of what worked.
How Can an Engineering-Led Supplier Support Complex NPI?
XINKEY MOULD supports short-run injection molding as part of an injection mold engineering workflow. The team starts with DFM analysis, wall thickness and draft review, and Moldflow analysis before tooling. It then connects precision CNC machining, EDM, mold assembly, trial molding, and low-volume production support.
For complex NPI, the useful detail is the handoff: T1 samples are checked against design intent, cooling and venting are reviewed against defects, and slider, lifter, insert, or threaded-core behavior is tested before a volume decision.
The process also covers rapid prototype mold development, pilot production, and bridge production, so procurement can compare a tool plan with a real launch schedule. See the injection mold engineering solutions and custom injection mold products pages for the relevant service scope.
FAQ
Q1: When should you choose short-run injection molding for NPI?
A: Choose it when fit, function, finish, assembly, or market timing needs evidence from production-intent parts before full-volume tooling.
Q2: Can low-volume injection molding use the final production resin?
A: Yes. Use the approved resin grade when the tool, press, and process window support it, then record material lot and drying conditions with the samples.
Q3: How do T1 samples help a procurement decision?
A: T1 samples connect the quoted tool design with measured dimensions, defects, cycle data, and open engineering actions, giving procurement a clear release gate.
Q4: Does a complex injection mold require Moldflow analysis?
A: Moldflow analysis is useful when gates, thin walls, multiple cavities, cooling balance, air traps, or weld lines create meaningful process risk.
Q5: What should you request before pilot production?
A: Request an approved drawing, resin specification, dimensional report, cosmetic standard, process settings, open-issue list, and a correction plan with owners and dates.
- 9th 10 月2026
原型注塑成型 vs 3D 打印 vs CNC 加工
选择原型制作工艺取决于您需要零件解答的问题。例如,用于装配检查的外壳、卡扣式盖子和十件试生产所需的证据各不相同。本指南从交付周期、材料性能、精度、表面光洁度、数量和采购风险等方面对原型注塑成型、3D 打印和 CNC 加工进行了比较。
每种塑料原型制作方法都能生产出什么样的产品?
这三种方法制造零件的方式各不相同,因此零件所承载的证据也各不相同。注塑成型是将熔融的热塑性塑料注入型腔,并重复相同的循环。3D 打印是逐层添加材料。CNC 加工是从实心块体上去除材料。您的预期用途应该决定哪种方式最为重要。
原型注塑成型
原型注塑成型使用小批量模具(通常为铝或较软的工具钢)来制造计划生产所需的树脂零件。您可以检查成型零件的熔接线、缩痕、翘曲、卡扣力以及表面纹理。
3D打印
3D打印适用于日常几何形状的改变或一到五个快速零件的打印。FDM技术可使用ABS、PLA和聚碳酸酯等材料;树脂和粉末系统则可实现更精细的细节。层方向会影响强度、阶梯状纹理和热响应。使用相同标称聚合物的3D打印铰链的弯曲性能可能与注塑成型的铰链不同。
数控加工
CNC加工从ABS、POM、尼龙、PC或其他工程塑料块上切割零件。它能提供清晰的基准面和精确的尺寸,尤其适用于易于加工的特征。内部通道、深腔和薄肋会增加成本,因为刀具需要操作空间和支撑。加工后的零件还会保留塑料块的纹理和刀痕,这可能与模压成型的纹理有所不同。
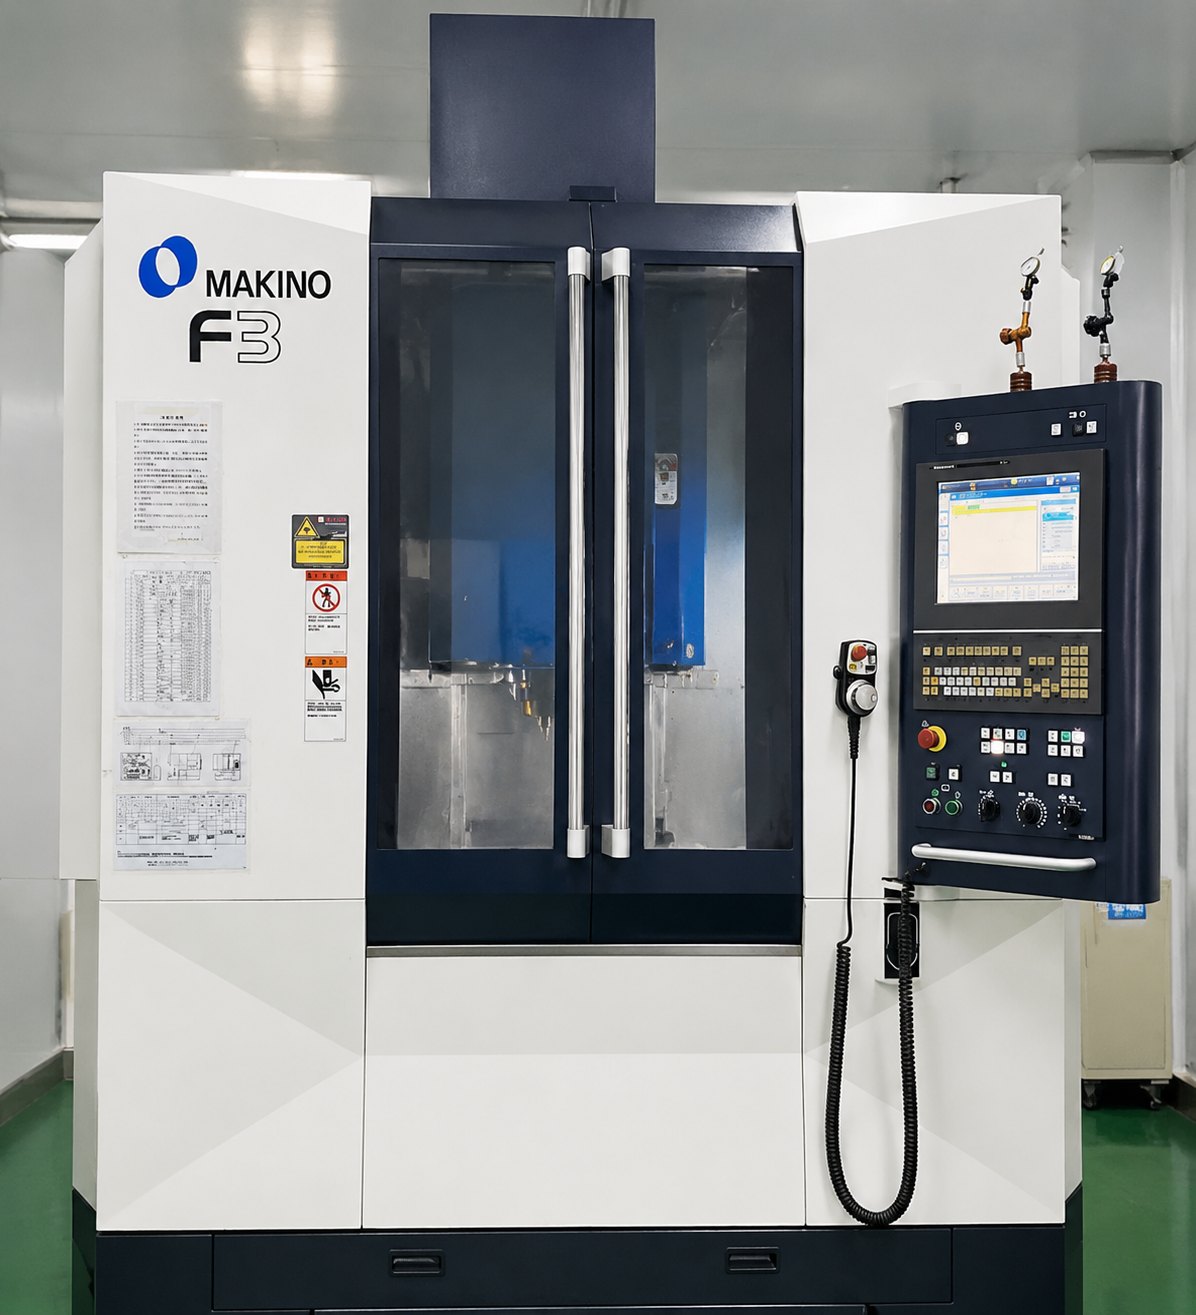
图片:数控铣床主轴雕刻白色塑料原型零件.webp
哪种方法最适合您的数量和交货时间?
数量会影响成本曲线。在比较报价之前,请设定目标数量、样品日期和设计修改次数。
一至十部分
3D打印适合早期形状检查,因为无需专用模具。CNC加工适合需要精确孔径、平面基准或功能性螺纹的零件。当决策涉及模塑件的性能时,例如活动铰链或夹子,注塑成型原型则更为合适。
十到几百份
小批量注塑成型可以将模具成本分摊到可重复生产的零件上,并支持使用生产级材料。过渡模具可以在准备更长寿命模具的同时提供试制件或可销售的成品。CNC加工适用于厚重、刚性零件;3D打印则增加了去除支撑、打磨或定向检测等功能。
进度计划
文件准备和排程完成后即可开始3D打印。CNC加工时间取决于编程、材料、夹具和表面处理。标准的快速模具项目大约需要两到四周才能完成T1样品;滑块、嵌件、拆卸系统、特殊钢材或高要求的表面处理可能会将制作周期延长至四到八周。请与供应商确认各个阶段的里程碑。
材料和零件性能对比如何?
材料的选择应根据使用条件而定,例如冲击、高温、化学品腐蚀、弯曲、外观或电绝缘性能。使用替代树脂会导致关键性能问题无法解决。
生产级树脂证据
注塑成型工艺可让您在可控的条件下测试ABS外壳、PC冲击部件、PP活动铰链、PA填充部件以及各种填充型材料。树脂干燥、熔体温度、保压压力和冷却都会影响收缩率和翘曲度。PP具有耐化学性和柔韧性;填充型PA可增加刚度,但会增加模具磨损。
印刷和机械加工材料的限制
打印部件可能存在空隙、层间接缝或强度不均匀等问题。CNC加工部件使用预制材料,但切割过程可能会暴露应力或导致薄壁变形。对于热老化、化学腐蚀或重复组装等情况,测试样品应与最终使用的树脂和工艺相匹配。
哪种方法能获得合适的精度和表面光洁度?
精度取决于每个特征的具体情况。基准策略、收缩率、工具使用、检测方法和热历史都会对其产生影响。
准确性和细节
CNC加工能够对可加工的表面和孔保持严格的公差,因此非常适用于量规和配合研究。数字化构建直接形成复杂形状,最终打印件保留了构建表面;模具分型线并不决定其几何形状。
小孔和边缘可能需要后处理。注塑成型工艺稳定后,型腔几何形状会重复出现;DFM(面向制造的设计)评审必须考虑拔模斜度、分型线、浇口、顶出和树脂收缩等因素。
表面处理和外观
机加工表面会留下刀痕,可以进行抛光或纹理处理。印刷表面通常需要打磨或蒸汽处理。模腔在每次注塑成型后都能保持特定的抛光或纹理效果。浇口痕迹、熔接线、顶出痕迹和光泽度差异都应在图纸上标明,尤其是在外露部件上。
购买对比中应该包含哪些内容?
有用的报价将价格和时间与明确的范围挂钩。比较工程量、材料、检验、修改、交付方式和单价。
报价清单
请提供三维模型、带尺寸标注的二维图纸、树脂牌号、颜色、表面处理、数量、年度预测、关键公差、装配环境以及所需的样品日期。请询问模具材料、型腔数量、流道类型、模具寿命目标、试模、T1报告、纠错政策以及所有权条款。
对于数控加工,请列出原材料、基准方案、检测点和表面处理工艺。对于印刷,请具体说明工艺流程、方向、层高、后处理工艺和受力方向。
DFM 和审判记录
面向制造的设计 (DFM) 和 DFM 分析应在金属切削前标记壁厚、拔模斜度、加强筋、凸台、倒扣、浇口、排气孔和顶出等问题。在 T0 和 T1 阶段,记录短射、飞边、烧焦、缩痕、熔接线、粘连、翘曲和尺寸偏差。将每个问题与相应的操作和负责人关联起来。该记录为采购部门批准下一模具或修改零件提供了明确的依据。
工程合作伙伴如何将原型结果与生产联系起来?
当原型机暴露出模具或工艺问题时,交接环节至关重要。设计逻辑应贯穿整个评审过程,包括模具修正、试模以及小批量生产决策。
XINKEY MOULD 将此工作流程应用于塑料零件开发。其工程师在模具制造前会审查壁厚、拔模斜度、收缩率、浇口、流道、冷却、排气、顶出和模具强度。对于侧孔、螺纹或双材料特征,其范围包括滑块、顶杆、镶件、螺纹型芯、自动脱模装置和 2K 双色注塑结构。CNC、EDM 和线切割等加工方式支持模具制造,加工控制精度可达 ±0.01 mm(在特征和检测方法允许的情况下)。
作为一家塑料注塑模具制造商,它将试验结果应用于模具修正和小批量注塑成型,并将样品数据与生产联系起来。
常问问题
问题1:对于20个零件来说,原型注塑成型值得吗?
是的,如果您严格要求使用生产级树脂、模压成型的夹子、铰链或特定纹理。只需权衡一下工具的前期成本与自行加工或打印每个零件的成本即可。还要考虑您对可靠、稳定的性能有多看重。
Q2:3D打印可以取代注塑成型原型吗?
只能说部分如此。3D打印在处理基本形状、间隙和早期人体工程学检查方面表现相当不错。然而,注塑成型则展现了截然不同的细节。它能精确地展示型腔填充过程,突出真实的收缩和潜在的熔接线。此外,它还能演示实际的脱模过程和树脂的真实性能。
Q3:何时才是CNC加工的实用选择?
当您只需要少量刚性零件,且对基准面、孔或螺纹的精度要求极高时,它就能发挥出色作用。对于体积较大的几何体,它也是明智之选。打印厚截面耗时过长。此外,小批量生产也无法抵消定制模具的成本。
Q4:最终塑料材料用于哪个工艺?
注塑成型通常使用预先设计好的树脂。数控加工依赖于标准工程塑料坯料。而3D打印则仅限于适用于特定打印机的聚合物。因此,在得出任何最终性能结论之前,务必核实热性能、化学性能和强度规格。
Q5:何时应该从原型模具过渡到生产模具?
只有在设计完全稳定后才能进行过渡。您的 T1 样品也必须通过所有基本验收标准。此外,您的预计产量必须足以支持购买寿命更长的模具。请根据原型运行的可靠数据做出明智的选择,这些数据包括:记录的周期时间、实际废品率、实际维护需求和已验证的单位成本。
- 2026年10月2日
快速原型注塑成型:塑料零件开发实用指南
CAD模型看起来可能已经完成,但注塑成型的零件仍然存在一些问题。加强筋会下陷吗?卡扣能经受住组装吗?外壳会围绕按钮变形吗?快速原型注塑成型技术使用预先设计的树脂制造出实际的注塑零件,从而解答这些问题。
该方法适用于需要进行功能测试、试生产、客户样品或早期销售样机的塑料零件开发。速度优势在于:在金属切削开始之前,就已明确了刀具的选择范围并完成了必要的工程设计工作。
什么是快速注塑成型?
快速注塑成型使用快速制造的模具来生产可重复的塑料零件。许多团队也称之为原型注塑成型或快速模具制造。该工艺遵循与生产成型相同的基本流程:夹紧、注射、保压、冷却、开模和脱模。
它与生产工具的区别
注塑模具原型通常使用铝、P20、NAK80 或更硬的嵌件来制作耐磨部件。数量、树脂、表面光洁度和公差是选择嵌件的关键因素。铝材适用于小批量生产。P20 便于焊接和设计修改,而 NAK80 则适用于抛光表面。
生产工具可能包含多个型腔、硬化钢材、热流道、自动化操作和可更换的易损件。快速模具可确保成型过程与当前测试目标保持一致。
何时应该使用快速模具?
当打印或机械加工的原型无法解答下一个工程问题时,应使用快速模具。模塑树脂在焊缝、活动铰链、卡扣配合、凸台和纹理壁等部位的性能会有所不同。
功能验证和试运行
使用生产级材料测试刚度、耐化学性、热响应或装配力。ABS 适用于坚固的外壳,PC 适用于抗冲击或透明部件,PP 适用于活动铰链,PA 适用于承载重物的组件。填充 PA 和耐高温等级的 PA 会快速磨损软性模具。
小批量注塑成型适用于试生产和小批量产品发布。过渡模具可在模具长期使用期间提供可销售的产品,并为买家提供可衡量的周期、废品和检验数据。
开发流程是如何运作的?
一个有效的流程始于零件需求。共享3D模型、2D图纸、树脂等级、颜色、表面处理、数量、关键尺寸和装配环境。标记密封面和外观区域。诸如“所有地方公差要求严格”之类的模糊说明会增加成本并留下争议空间。
模具设计前进行可制造性设计
可制造性设计 (DFM) 检查壁厚、拔模斜度、倒扣、加强筋、凸台、分型线、浇口、排气孔和顶出。DFM 分析还应识别跨越分型线的尺寸以及需要滑块、升降器、嵌件、套筒或旋出机构的特征。
壁厚约为 1.5 至 2.5 毫米的部件适用于许多常见的热塑性塑料,但树脂供应商的产品范围和部件的功能是首要考虑因素。相邻壁的厚度应尽量接近。较厚的凸台底座冷却速度较慢,可能会导致对面出现明显的凹陷。拔模斜度有助于部件脱模;纹理表面通常比抛光表面需要更大的拔模斜度。
流动模拟可以测试浇口、流道平衡、熔接线、气穴、压力和热行为。它适用于薄壁、长流道、多腔模具和外观零件。每项发现都应指导相应的改进措施,例如移动浇口或修改冷却通道。
工具构建、试用和修正
CNC加工可形成大多数型芯和型腔。电火花加工可处理深槽、锋利的内部细节以及刀具无法精确加工的几何形状。线切割、研磨、装配和抛光等工序则可完成工具的最终加工。
T0 检查填充、开启、顶出和安全操作。团队记录短射、飞边、烧焦、缩痕、熔接线、翘曲、粘连和尺寸偏差。T1 样品应包含约定的树脂、工艺记录、尺寸报告和剩余步骤。即使是来自不稳定循环的漂亮样品,也仍然是未完成的结果。车间经常会吸取这样的教训。
哪些设计选择决定了零件质量?
零件质量取决于一系列相互关联的决策。浇口位置影响熔接线和包装。冷却影响循环时间和翘曲。顶出影响拖痕、泛白和变形。
闸门、冷却、排气和喷射
将浇口设置在熔体能够以可控压力填充型腔并压实较厚区域的位置。在多型腔模具中,平衡的流道至关重要,因为一个型腔过早填充会分散另一个型腔的压力。流道末端的排气孔可以排出滞留的空气,减少烧伤。
冷却通常占据注塑成型周期的大部分时间。型芯和型腔周围的冷却层需要均匀覆盖。局部过热会导致部分区域保持柔软,而邻近区域的塑料收缩,这可能导致脱模后扁平外壳发生扭曲。因此,顶针、顶套、脱料板、顶杆或气动顶出装置需要足够的接触面积,才能在不造成凹陷的情况下移动零件。
下单前应该检查哪些内容?
按范围比较报价。最低的模具费用报价意义不大,因为报价范围可能很广。mits树脂、试验、检验、变更或预期工具寿命。
实用采购清单
请各注塑模具制造商详细说明模具材料、硬度、型腔数量、流道类型、模具寿命、包含的试模次数、T1交货期、尺寸报告、维护计划和所有权条款。确认注塑机吨位和注射量。较大的注塑面积需要足够的锁模力来控制飞边。
比较不同数量的零件成本。冷流道适用于许多小批量生产,但每次注塑都会产生流道材料。热流道可以减少浪费,并可能缩短生产周期,但模具和维护成本更高。产量和树脂价格是选择流道的关键因素。
首次试模后,预留一次修正循环的时间。标准快速模具大约需要两到四周才能达到 T1 阶段。复杂的螺纹拆卸、嵌件或双材料结构可能需要四到八周。几何形状、钢材供应、表面处理和检验范围都可能导致交付日期变更,因此制定里程碑计划比一次性交付承诺更有用。
将原型结果转化为生产决策
试验报告应将每项缺陷与具体操作和责任人关联起来。这样的记录能将快速检测工具转化为切实可行的生产关卡。
XINKEY MOULD 通过早期可制造性设计 (DFM)、模流分析、快速原型模具开发、试模和过渡生产,为这一阶段提供支持。其工程范围涵盖滑块、顶杆、镶件、螺纹型芯、冷热流道、平衡顶出以及冷却布局,适用于需要比简单开合式模具更复杂功能的零件。精密加工包括数控加工 (CNC)、电火花加工 (EDM) 和线切割,加工控制精度可达 +/-0.01 毫米,具体取决于特征和检测方法。
团队可以将试验结果应用于模具修正和小批量零件生产,从而确保设计反馈、模具变更和工艺记录之间的关联性。对于采购方而言,这种连续性使得T1评审更易于审核,并为生产模具决策提供更可靠的成本和质量依据。
常问问题
问题1:快速原型模具生产T1样品的速度能有多快?
答:标准工具大约需要两到四周才能达到T1标准。滑块、旋出系统、嵌件、双材料结构、特殊钢材或要求高的表面处理可能会将工期延长至四到八周。
Q2:快速注塑模具一次可以生产多少个零件?
答:模具寿命取决于模具材料、树脂、压力、温度、几何形状和维护情况。报价前请确定所需的注塑次数,以便模具制造商选择合适的钢材并保护高磨损区域。
Q3:可以使用最终生产用的树脂吗?
答:是的,在很多项目中都是如此。使用指定的树脂能更好地检验其贴合性、强度、收缩率、热响应和表面质量。对于磨蚀性、腐蚀性或耐高温等级的树脂,可能需要使用钢制嵌件或钢制工具。
Q4:询价时需要发送哪些文件?
A:请提供 3D 模型、带尺寸标注的 2D 图纸、树脂等级、颜色、表面处理、数量、年度预测、关键公差、装配细节以及所需的样品日期。
Q5:何时应该过渡到生产模具?
答:当设计稳定、试验符合验收标准且预测产量支持使用长寿命模具时,即可考虑推进。决策时应参考原型运行中测得的周期时间、废品率、维护需求和单位成本。



联系我们