

What Is Considered Low-Volume Production? Batch Sizes, Quantities & Industry Benchmarks
-
 autor
- 29th October 2026
What Counts as Low-Volume Production?
Low-volume production usually means about 10 to 10,000 parts in one planned run. Use that range to frame low-volume production quantities, then adjust it for industry, material, process, and qualification work. The same low-volume production volume can mean very different things in medical and consumer programs.
A Practical Quantity Range
Use these bands as planning references. They describe a product stage; applicable rules set legal and regulatory definitions.
| Stage | Working quantity | Main purpose |
| Prototype | 1 to 10 | Form, fit, and early function |
| Low-volume production | 10 to 10,000 | Validation, launch supply, or specialized demand |
| Produção em massa | 10,000 and above | Stable demand and dedicated capacity |
O low-volume manufacturing batch size also depends on release timing. Five hundred units delivered once differs from five releases of 100. Forecast accuracy, storage, cash flow, and revision risk shape that choice.
Batch Size, Annual Volume, and Program Volume
Keep three figures on the purchase request: units per release, expected annual demand, and lifetime demand. A project may need 500 units for a first shipment and 2,000 across the year while the tool changes. That remains small-batch manufacturing with staged releases.
Which Industry Benchmarks Fit Your Batch Size?
Low-volume manufacturing benchmarks frame a quote and validation plan. Your forecast, regulatory plan, and supplier capacity review set the final range.
Planning Bands by Industry
| Indústria | Illustrative run | What sets the band |
| Medical and laboratory equipment | 10 to 500 | Traceability, qualification, and controlled design changes |
| Aerospace and defense components | 10 to 1,000 | Complex geometry and first-article work |
| Industrial equipment and automation | 50 to 5,000 | Project orders, replacement demand, and service parts |
| Automotive specialty and aftermarket parts | 100 to 10,000 | Platform life, tool life, and customer approval |
| Consumer electronics and smart hardware | 500 to 10,000 | Market pilots, cosmetic standards, and product revisions |
| Packaging and household products | 1,000 to 10,000 | Resin cost, cavity count, and unit economics |
A 300-unit medical run can be a major validation build, while 5,000 electronics units can remain a market test. Product risk and approval work give quantity its meaning.
How Does Low-Volume Production Compare with Other Stages?
Purpose defines the stage. A prototype answers design questions, a pilot checks the process and work instructions, and a bridge run supplies customers while a higher-volume tool is completed.
Prototype, Pilot, and Bridge Production
Prototype parts can use a temporary process or substitute material. Pilot production uses the intended process, inspection method, packaging, and operator steps. Set the pilot production quantity from the test plan: 50 parts may cover an assembly study, while several thousand may support a launch build.
Bridge production carries approved material, drawing revision, and process settings into an early shipment. It gives you time to qualify a hardened tool or higher-cavity layout. Keep a clear record so the next tool uses those lessons.
When Mass Production Starts
Mass production starts when demand stays steady, revisions are controlled, quality data repeats, and unit economics support dedicated tooling. The threshold varies by product.
How Does Batch Size Affect Cost and Purchasing?
Batch size spreads fixed engineering and tooling costs across parts. It also sets inventory exposure and the number of design changes you can absorb.
Fixed Tooling and Unit Cost
Use this simple planning formula:
estimated unit cost = recurring part cost + (tooling and engineering cost / planned units)
Add freight, inspection, scrap, qualification, storage, and engineering changes when comparing quotes. These costs can outweigh a small piece-price difference.
The useful manufacturing quantity breakpoints for a quote may be 100, 500, 1,000, 5,000, and 10,000 units. Ask for each price at the same drawing revision, material grade, inspection scope, and delivery term.
Production Batch Size Planning
Production batch size planning starts with demand and ends with a release gate. Ask for minimum order, staged-release terms, tool ownership, cavity plan, shot count, packaging, and maintenance. A large order ties cash to a changing design; a very small order spreads tooling cost across too few parts.
When Does Low-Volume Injection Molding Fit?
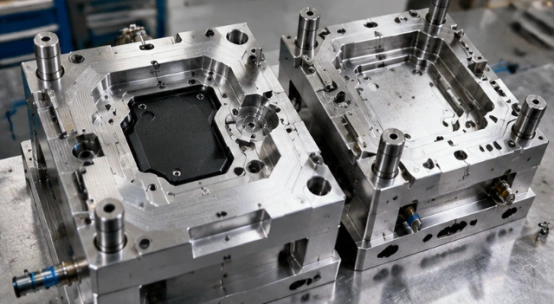
Moldagem por injeção de baixo volume fits repeatable plastic parts in the hundreds or thousands when you need production-intent resin, stable cosmetics, and measured dimensions. Match tool structure to the forecast and design-change rate.
Tool Choice, Tool Life, and Cavity Count
Single-cavity or low-cavity tooling leaves room for early changes. Multi-cavity tooling lowers piece cost after geometry, resin, and assembly settle. Aluminum or soft steel suits an early run when tool life and resin conditions fit; hardened steel suits higher shot counts. Review tool life and cavity count against cycle time and demand.
Engineering Checks Before Steel Cutting
Start with DFM analysis. Check wall thickness, draft, parting line, shrinkage, undercuts, tolerances, cosmetic zones, and ejection. Uneven walls create sink or warpage; gate errors create flow marks, air traps, or weld lines.
Usar Análise Moldflow for risks around gate position, runner balance, thin walls, cooling, or multi-cavity filling. Review sliders, lifters, inserts, threaded cores, mold strength, cooling, vents, and ejection before machining. T0 trials expose small details quickly.
What Should You Ask a Supplier Before Ordering?
The quote should end with records and owners. Price alone cannot show whether the batch will pass assembly or repeat across a longer run.
T1 Evidence and Quality Gate
Request T1 samples with resin lot, machine settings, mold temperature, pressure, cycle time, cavity ID, dimensions, cosmetic photos, and open actions. Set CTQs, part weight, flash and sink limits, and assembly tests before the run. Name the approver and correction date.
Procurement Questions
Ask for DFM timing, mold release, steel and heat-treatment details, T0 and T1 dates, correction rounds, pilot support, and the bridge production handoff. Compare two or three quotes against identical CAD data and material specifications.
When Should You Increase Production Volume?
Scale when the current tool, supplier, or release pattern reaches a measured limit. Consider a new tool when demand exceeds capacity, wear changes dimensions, cycle time misses the cost target, or a design freeze supports investment.
Carry the approved CAD revision, resin, Moldflow findings, T1 data, process window, and maintenance record into the next tool. This record anchors the next estimate.
Which Engineering Support Fits Your Low-Volume Production Plan?
Once the quantity plan reaches plastic tooling, XINKEY MOULD can connect the engineering handoffs in a low-volume injection molding run. The workflow covers DFM analysis, Moldflow analysis, mold structure, machining, cooling, venting, ejection, and trials.
Sliders, lifters, inserts, threaded cores, and runner systems can match the release size and change rate. T0 and T1 verification records the drawing revision, resin, and acceptance data for pilot or bridge production. Review the injection mold engineering solutions and custom plastic injection molds pages when requesting a quote. Include cavity count, steel, shot-life target, and T1 deliverables.
Perguntas frequentes
Q1: What Is Considered Low-Volume Production?
A: A common planning range is 10 to 10,000 parts per run. Industry, process, material, and qualification work set the practical boundary.
Q2: How Do You Choose Low-Volume Production Quantities?
A: Combine the first-release need, annual forecast, validation plan, storage limit, revision risk, and supplier capacity.
Q3: Is 1,000 Units a Low-Volume Production Volume?
A: It can be. One thousand units may support a large medical validation program or an early consumer product launch.
Q4: What Should T1 Samples Include?
A: Request the resin lot, machine settings, cavity identification, dimensions, cosmetic photos, sample count, and open corrective actions.
Q5: When Does Low-Volume Injection Molding Make Sense?
A: It fits repeatable plastic parts in the hundreds or thousands when production-intent resin, dimensional control, and a path to bridge or higher-volume production matter.
For a project review, share the CAD file, resin, CTQs, first-release quantity, annual forecast, and target date. The quantity decision becomes much clearer when the tool plan and acceptance data sit in the same document.










Contacte-nos